How can SmartSense food safety monitoring improve operational efficiency and asset management in high-volume food production?
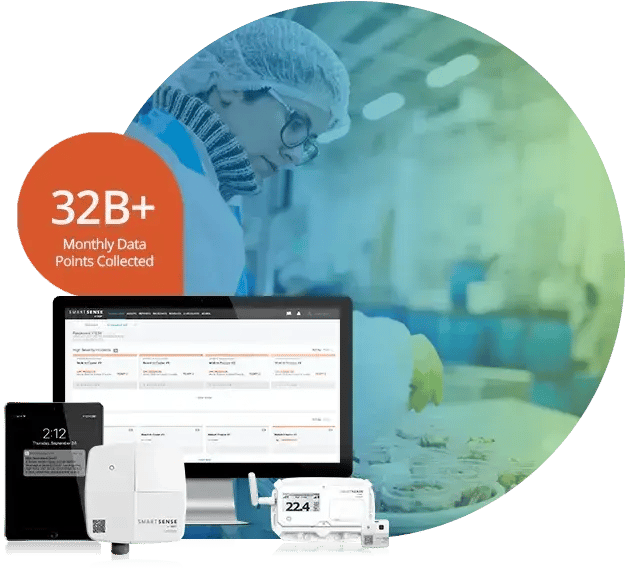
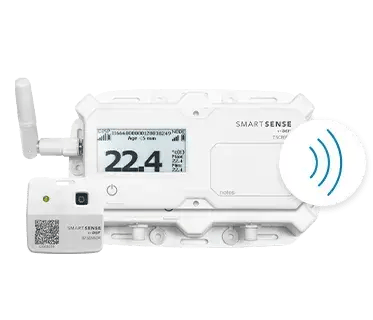
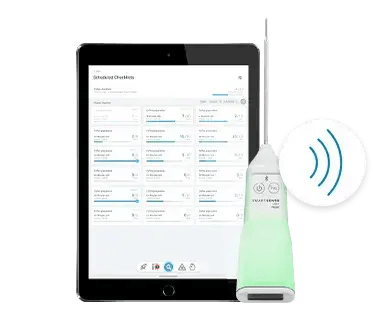
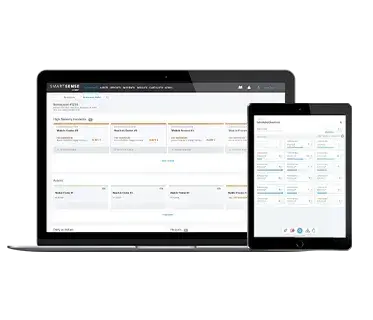
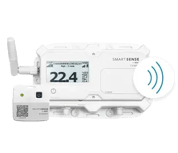
In high-volume food production facilities, thousands of units move through refrigerators, freezers, pasteurizers, and conveyors every hour, leaving little room for error. IoT-enabled food safety monitoring from SmartSense provides real-time alerts for temperature deviations, equipment malfunctions, or process anomalies, enabling teams to act immediately before disruptions escalate.
By integrating these refrigeration asset health insights with other existing asset management practices, food production facilities can maintain continuous operations, extend the life of critical equipment, and ensure consistent product quality across rapid, large-scale production lines.
Why are predictive signals critical for reducing risk in food production environments?
In complex, high-volume food production, small deviations like a rising refrigerator temperature or a slowing conveyor can quickly escalate into product safety issues or costly recalls. Predictive signals from IoT-enabled monitoring identify these anomalies before they become critical, allowing teams to take corrective action proactively. By detecting patterns and trends across equipment, storage, and production lines, food safety professionals can prevent contamination, maintain regulatory compliance, and protect both brand reputation and operational continuity in complex, multi-site production environments.
How does prescriptive analytics enhance traceability and batch-level decision-making in food production?
A deviation in equipment like a refrigeration unit, blast chiller, or pasteurizer can affect one or more batches of product during the food production process. SmartSense combines prescriptive analytics with cellularly-enabled IoT monitoring to provide actionable guidance whenever such deviations occur.
This asset monitoring adds intelligence to the batch-level and lot-level tracking that food production companies must engage in for end-to-end traceability. Real-time recommendations guide staff on corrective actions, ensuring regulatory compliance, traceability, and product safety while reducing waste, preventing recalls, and maintaining consistent quality across multi-line, multi-site operations.
Why is SmartSense capable of operating at scale across multi-site food production environments?
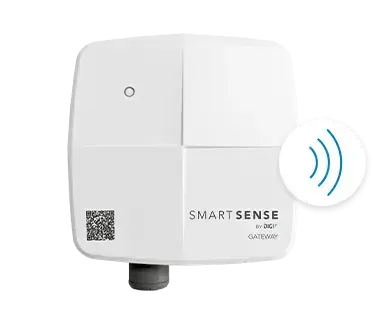
High-volume food production facilities and enterprise brands require a monitoring solution that can reliably operate across thousands of assets without compromising safety, compliance, or data integrity. SmartSense leverages cellular connectivity, reducing dependence on local Wi-Fi and ensuring uninterrupted, real-time data flow across distributed operations.
With years of analytics history and a proven track record supporting major brands, SmartSense provides the insights needed to manage compliance, operational efficiency, and risk at scale. The platform also adheres to industry standards, including SOC 2 Type II compliance, giving organizations confidence that sensitive operational and production data is secure.
This combination of technology, experience, and compliance capabilities makes SmartSense uniquely equipped to deliver enterprise-wide food safety visibility and actionable guidance across complex, multi-site food production environments.